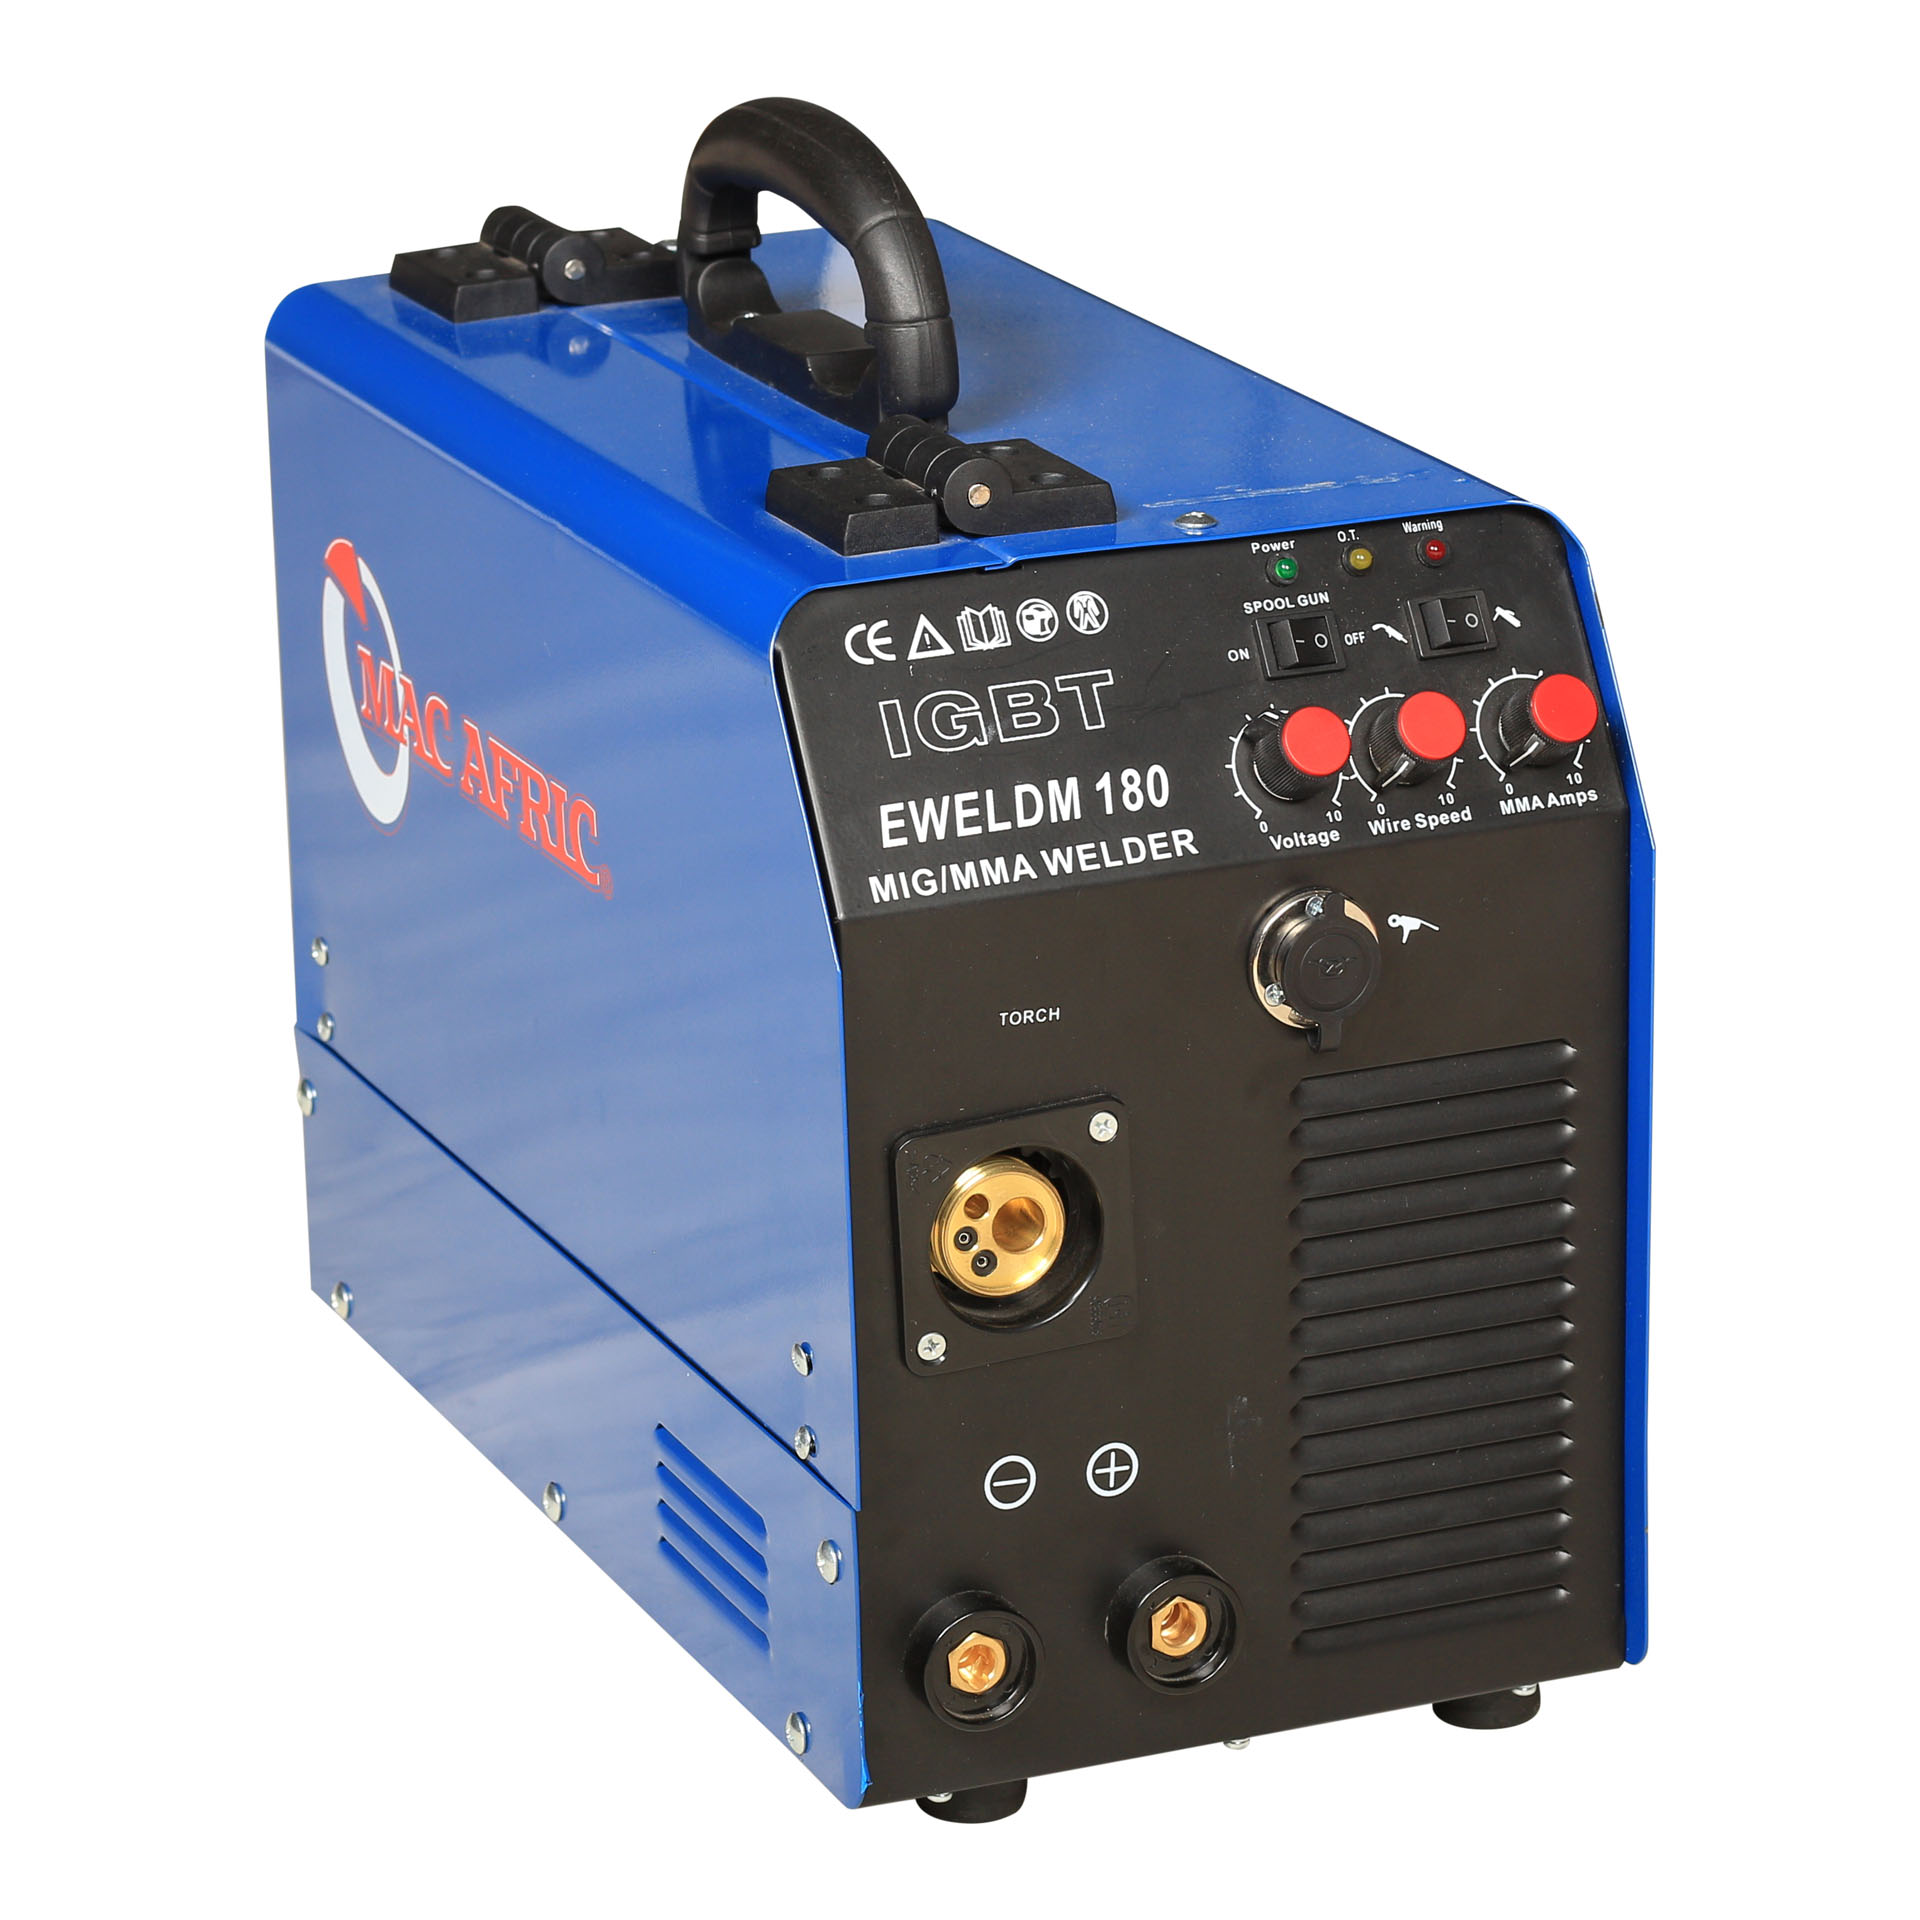
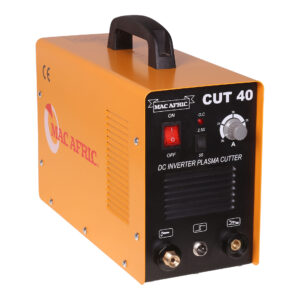
MAC AFRIC 180 A IGBT (MIG & MMA) Welding Machine
Description
Technical Specifications
Input Voltage: 230 V @ 50 Hz
Rated Input Current: 30 A
No-Load Voltage: 55 – 75 V
Output Current: 30 – 180 A (MIG / MAG), 15 – 160 A (MMA)
Duty Cycle: 180 A / 23 V @ 35%
150 A / 21.5 V @ 60%
120 A / 20 V @ 100%
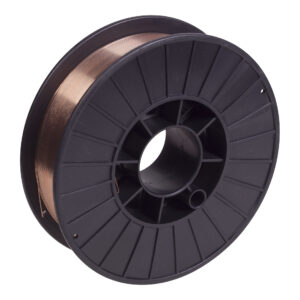
Suitable Wire Diameter: 0.6 mm, 0.8 mm
Key Features
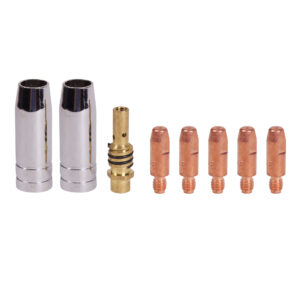
Includes MIG torch and earth clamp
Supports both MIG and ARC (MMA) welding
Reliable IGBT technology
Compact and portable design
Allows polarity changes for flux-core wire welding
MIG Welding Settings
MaterialWire TypeWire DiameterVoltageWire SpeedGas TypePolarity
Mild Steel: ER70S-6 Solid Wire: 0.8 – 1.0 mm: 16–19 V: 5 – 7: CO₂ or Argon/CO₂ Mix: DCEP (+)
Stainless Steel: ER308L Solid Wire: 0.8 – 1.0 mm: 18–20 V: 5 – 6.5: 98% Argon + 2% CO₂: DCEP (+)
Galvanised Steel: ER70S-6 Solid Wire: 0.8 mm: 15–18 V: 5 – 6: CO₂ or Argon/CO₂ Mix: DCEP (+)
MMA (Stick) Welding Settings
MaterialElectrode TypeRod SizeAmperagePolarityNotes
Mild Steel: E6013: 2.5 mm: 90 – 100 A: DCEP (+): All-position, easy to use
Mild Steel: E6013: 3.2 mm: 110 – 125 A: DCEP (+): For thicker steel
Stainless Steel: E308L-16: 2.5 mm: 85 – 100 A: DCEP (+): For tanks and pipes
Cast Iron: E7018 / ENiFe-CI: 3.2 mm: 100 – 120 A: DCEP (+): Preheat recommended
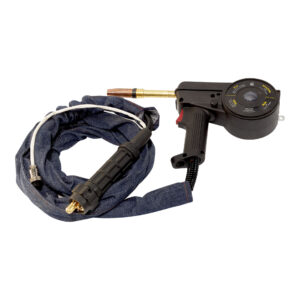
Spool Gun Setup (Optional for Aluminium)
MaterialWire TypeWire SizeVoltageWire SpeedGas TypePolarityNotes
Aluminium: ER4043 / ER5356: 1.0 mm: 18–22 V: 6 – 8: 100% Argon: DCEP (+): Use spool gun mode; keep cable straight
Setup Tips
Always use clean and dry wire or rods
Use proper drive rollers for MIG
Clamp on bare, clean metal for MMA
Shield from wind when using gas
Avoid exceeding 5–6 minutes continuous weld at high amps
Troubleshooting FAQ
IssueLikely CauseRecommended FixPro Tip
No arc: Loose clamp, low amps: Clamp to clean metal, increase amps: Always ground to bare, unpainted metal
Electrode sticks: Low amps, dirty metal: Use 90–100A, clean surface: Use E6013 for easy restarts
Arc pops or cuts out: Loose terminal, poor rod angle: Tighten cables, use correct angle: Store rods in sealed container
Breaker trips: Overload or poor socket: Use 20A+ socket, rest machine: Never use long extensions
Turns on but no weld: Blown fuse or PCB fault: Check lights, get technician check: Use surge protector
Weak weld: Low amps, wrong polarity: Use 90–125A, correct polarity: Keep consistent bead speed
Excessive spatter: Long arc, dirty base: Shorten arc, clean metal: 15° rod angle helps
Overheat light: Overuse beyond duty cycle: Rest 10–15 min, lower output: Use in shaded, ventilated area
Reviews
There are no reviews yet.