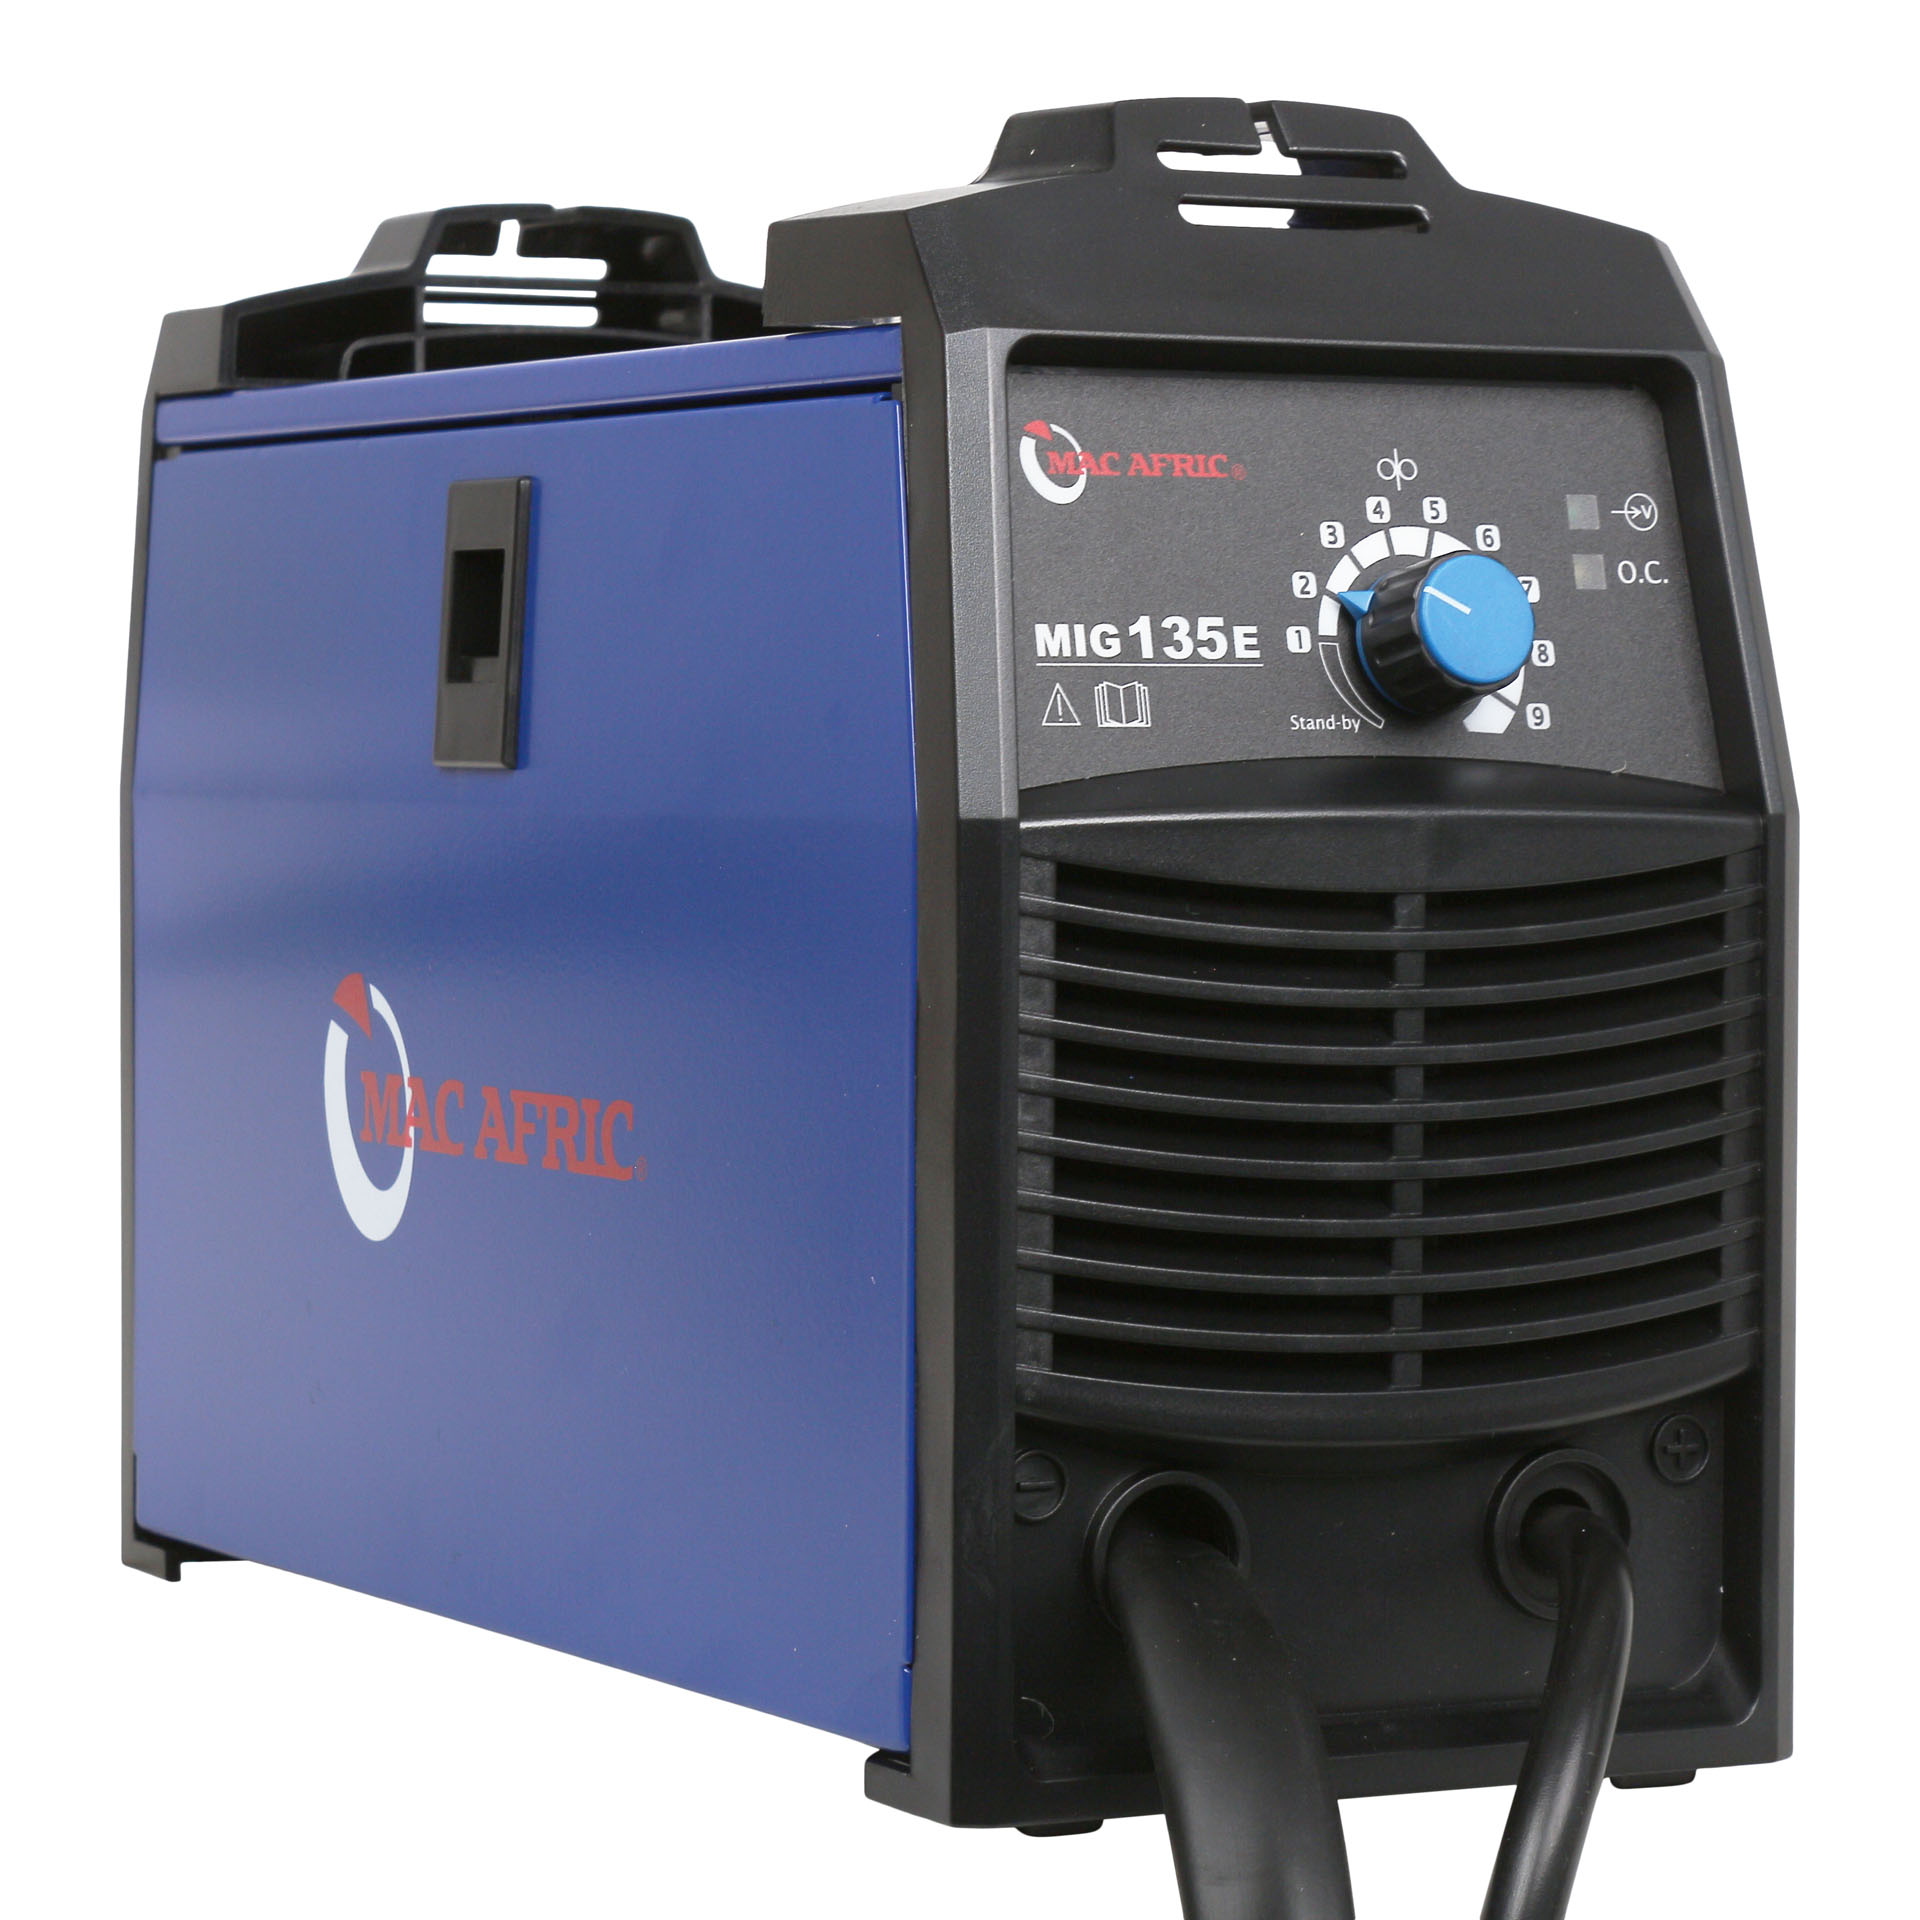
MAC AFRIC MIG135E Flux-Cored Welder (No-Gas Welder)
Description
Technical Specifications
Input Voltage: ±15% 220 ~ 240 V
Frequency: 50 / 60 Hz
Max Rated Input Current: 14 A (1EFF = 6.3 A)
Output Current @ Voltage: 40 A / 16 V – 100 A / 19 V
Wire Diameter: 0.6 – 0.8 mm / 0.9 mm (Flux-Cored Wire)
No-Load Voltage: 56 V
Duty Cycle @ 40°C: 20% @ 90 A / 100% @ 42 A
Power Factor: > 0.70
Efficiency: > 80%
Housing Protection Grade: IP21S
Insulation Grade: F
Troubleshooting & Quick Fixes
IssueLikely CauseRecommended FixPro Tip
No arc or wire feed: – Loose ground
– Trigger failure
– Broken contactor: – Clamp to clean metal
– Test trigger signal
– Check power switch & fuse: Pull trigger and listen for wire motor
Wire burns into tip: – Wire speed too low
– Wrong polarity
– Tip too tight: – Increase wire speed
– Ensure machine is on DCEP
– Use proper size tip: Replace tips often – flux-core is messy
Excessive spatter: – Wire speed too high
– Dirty metal
– Poor stickout control: – Reduce wire speed slightly
– Clean weld zone
– Maintain 10–15 mm stickout: Keep torch angle at 15° drag
Porous or weak weld: – Long arc length
– Fast travel
– Contaminated wire: – Shorten arc to ~5 mm
– Slow down travel
– Store wire dry & sealed: Wipe wire before loading spool
Machine shuts down mid-weld: – Overheating
– Exceeded duty cycle: – Let it cool for 10+ minutes
– Lower output settings: Operate in shaded, well-ventilated space
Inconsistent wire feed: – Liner clogged
– Drive roller tension incorrect: – Clean or replace liner
– Adjust tension on feed system: Don’t exceed 1m torch cable bend radius
Poor penetration: – Voltage too low
– Travel too fast: – Increase voltage
– Use weave technique on thick metal: Tack both sides before full pass
Frequently Asked Questions
Which welder is best for beginners?
Flux-core MIG welders like the EWELDM135 are excellent for beginners due to their simplicity and ability to weld without shielding gas.
What equipment do I need to start welding?
You will need a welder, helmet, gloves, safety clothing, and wire spools. This unit uses 0.6–0.9 mm flux-core wire.
Why does my weld look rough or porous?
This is often due to long arc length, fast travel speed, or contaminated wire. Follow proper prep and weld techniques to improve results.
What causes weld spatter?
High wire speed, dirty metal, or incorrect torch distance can all lead to spatter. Clean your material and adjust settings accordingly.
Why does my welder trip the power?
Overload or incorrect voltage input can cause this. Ensure the machine is plugged into a dedicated 220–240V outlet and not overloaded.
Reviews
There are no reviews yet.