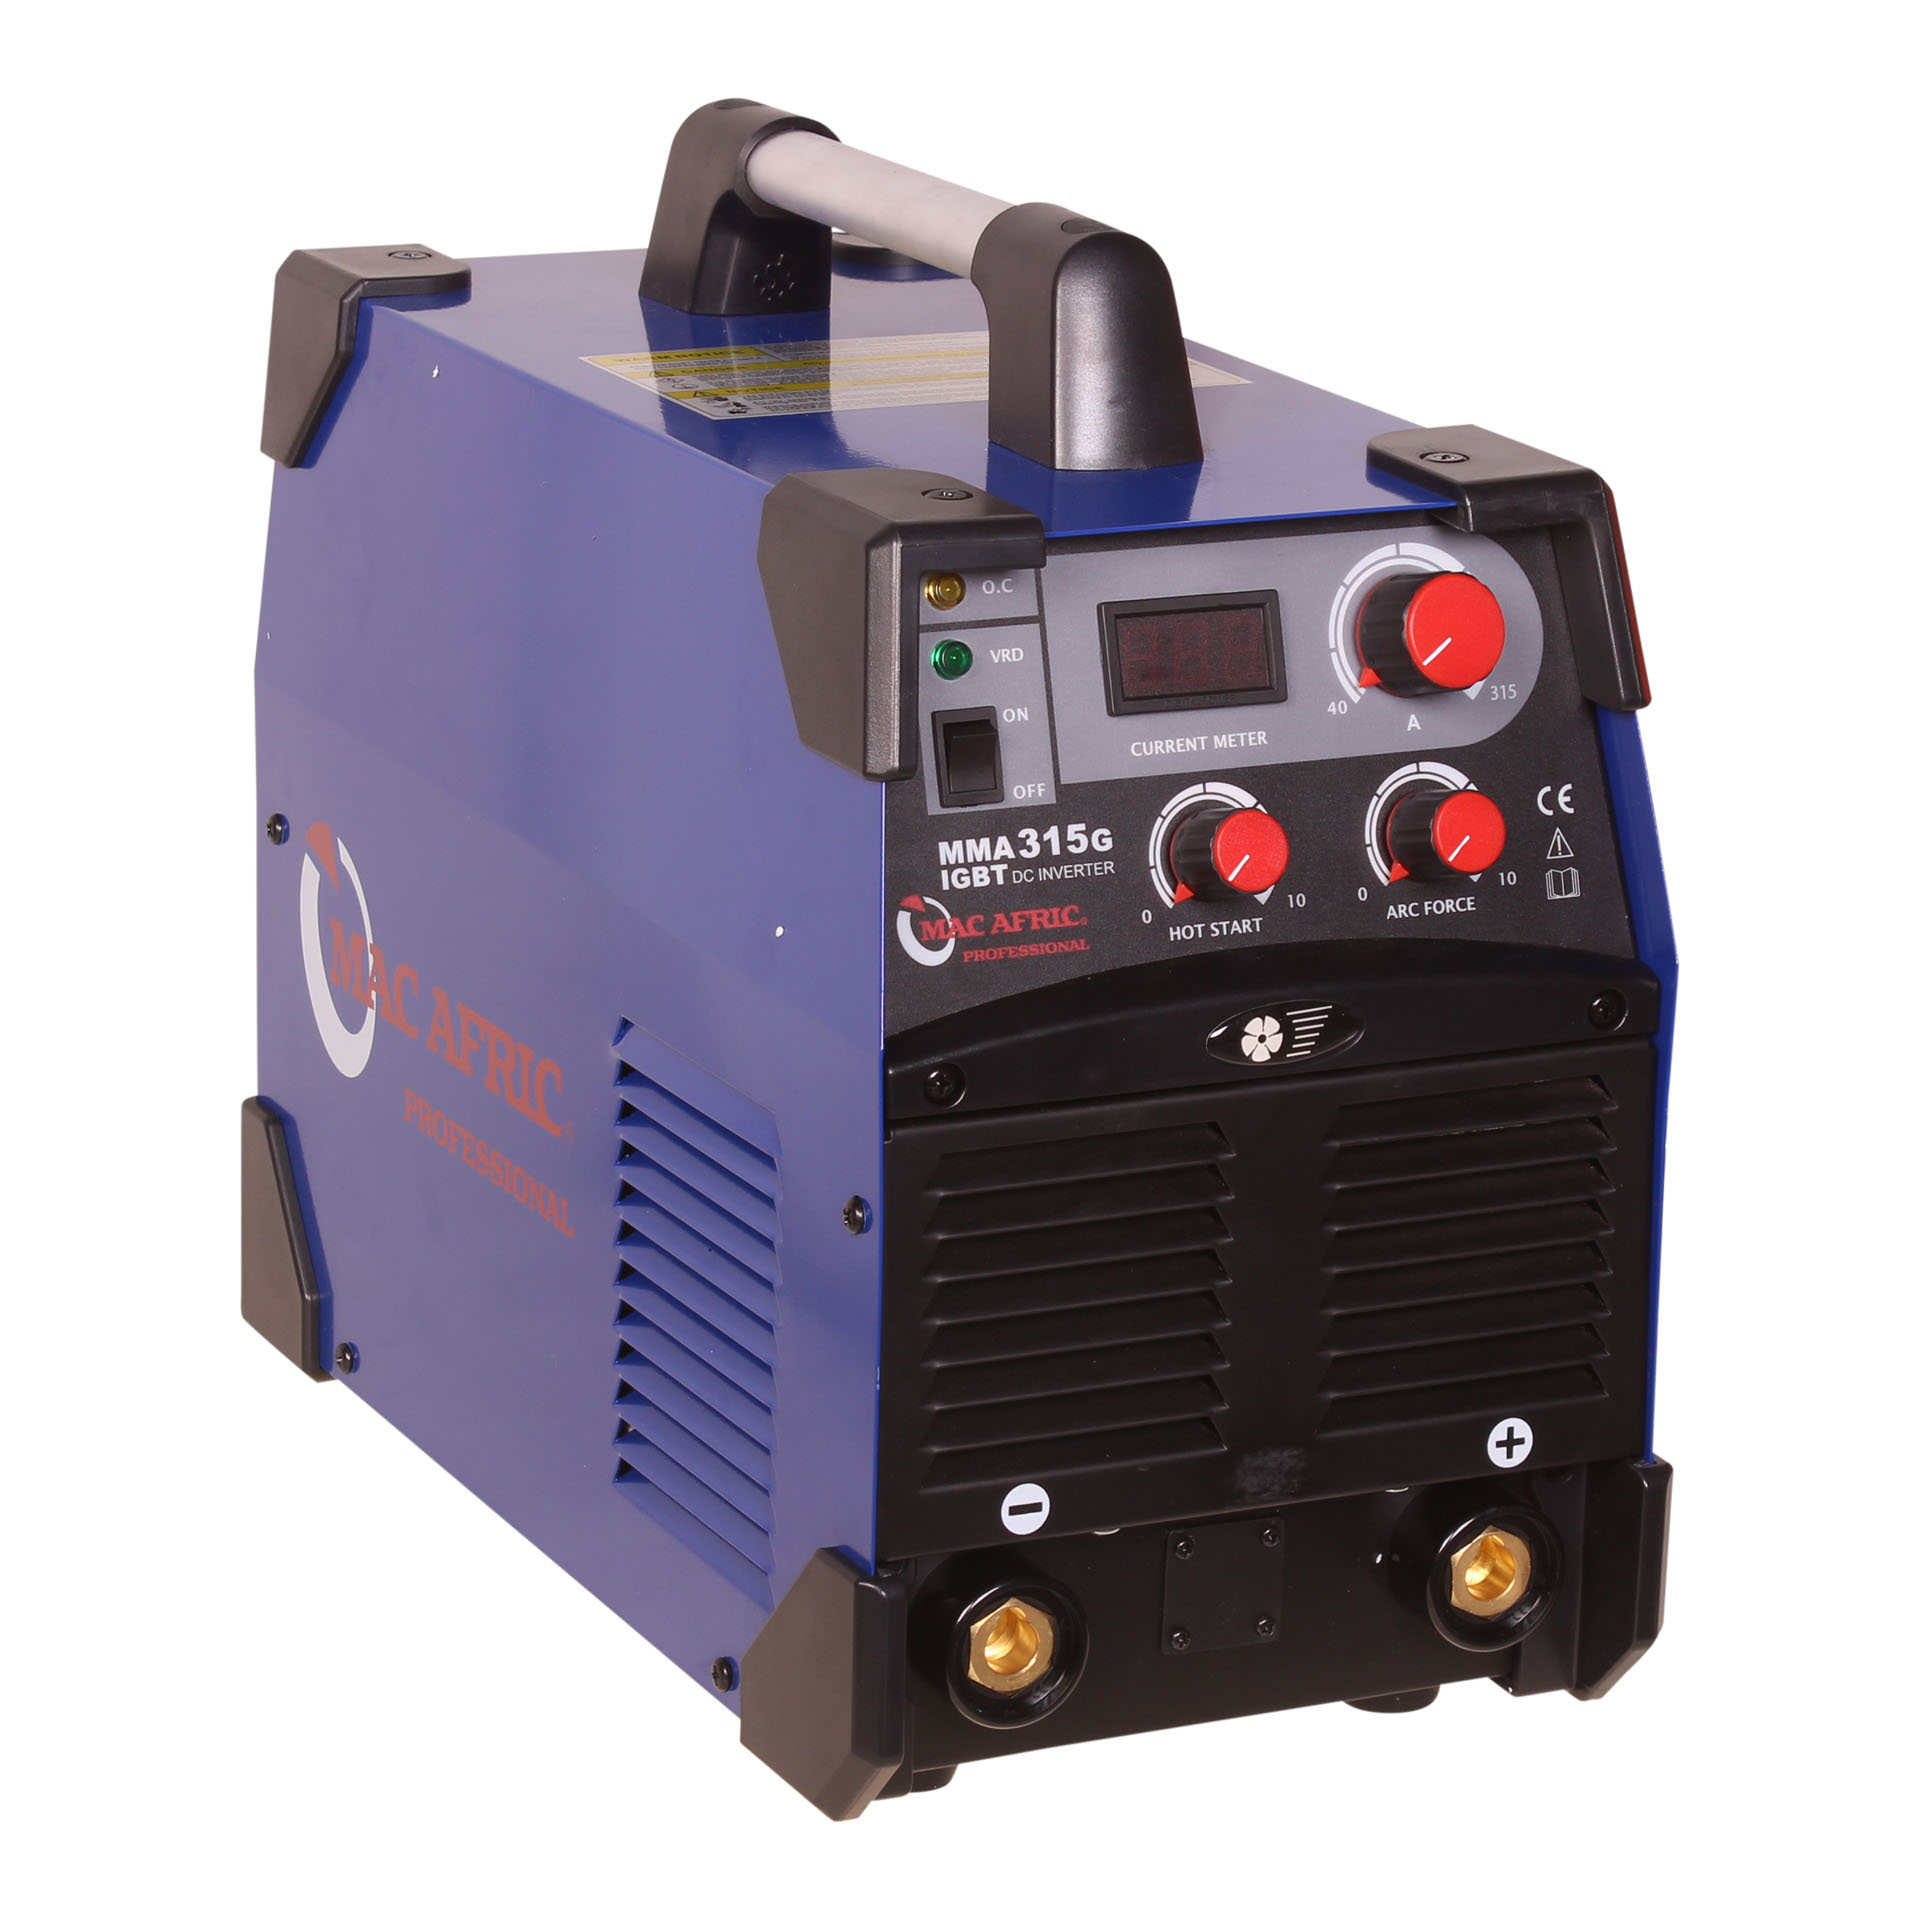
MAC AFRIC MMA D.C Model 315 G IGBT Inverter Welder
Lightweight, yet durable design, IGBT Inverter Technology offers an excellent duty cycle and efficiency. This machine is ideal for commercial use. This welder is fitted with both “ARC FORCE” and “HOT START” settings allowing further control of the weld characteristics. Appropriate for professionals but very easy for newcomers to learn.
Description
Technical Specifications
Input Voltage: 3P – 380 V ±15%
Frequency: 50 / 60 Hz
Rated Input Current: 17 A
No-Load Voltage: 65 V
VRD: 17.8 V
Output Current: 40 – 280 A
Hot Start Current: 0 – 135 A
ARC Force Current: 0 – 100 A
Duty Cycle @ 40°C: 280 A @ 40%
180 A @ 100%
Power Factor: >0.93
Efficiency: 85%
Housing Protection Grade: IP21
Key Features
Powerful 280A output for industrial applications
Built-in Hot Start and ARC Force controls
Wide compatibility with electrodes: 6013, 7018, stainless, cast iron
Stable arc with VRD safety feature
Efficient design with 85% efficiency and high duty cycle
IP21 protection grade for added safety in workshop environments
Troubleshooting Guide
Machine Not Powering On: Check power source (380V), fuses, and internal connections.
Electrode Sticking: Increase current, ensure good ground, and use dry rods.
Excessive Spatter: Reduce amperage, verify correct polarity, and maintain short arc length.
Poor Penetration: Increase current, reduce speed, or use correct electrode type.
Overheating: Let the unit cool, clean vents, and respect duty cycle limits.
Arc Cutting Out: Tighten all cable connections and inspect holder and internals.
Recommended Stick Welding Settings
Electrode TypeElectrode SizeAmperage RangePolarityApplication Notes
E6013: 2.5 mm: 70 – 100 A: DCEP: Light fabrication, thin steel
E6013: 3.2 mm: 100 – 130 A: DCEP: General steel welding
E6013: 4.0 mm: 140 – 180 A: DCEP: Medium-thickness sections
E6013: 5.0 mm: 180 – 220 A: DCEP: Thicker plate work
E7018: 3.2 mm: 110 – 140 A: DCEP: Structural, pressure vessels
E7018: 4.0 mm: 150 – 190 A: DCEP: Heavy structural steel
E7018: 5.0 mm: 190 – 240 A: DCEP: High-strength applications
Cast Iron (Nickel Rod): 3.2 mm: 90 – 120 A: DCEN: Repairs, low heat input
Stainless Steel Rod: 3.2 mm: 90 – 130 A: DCEP: Stainless steel welding
Quick Welding Tips
Keep arc length equal to rod diameter for best control.
DCEP is standard for general-purpose rods (6013, 7018).
Use lower amps and smaller rods for thin metals.
Bevel thick steel and use multi-pass with 4.0 or 5.0 mm rods.
Store electrodes in dry conditions to prevent moisture damage.
FAQs
Which welder is best for beginners?
Stick (ARC) welders like the EWELDS315 are suitable for beginners due to their simplicity, portability, and affordability.
Why does my electrode stick?
This can happen due to low amperage, poor grounding, or using damp electrodes. Increase current and ensure clean, dry materials.
What causes weld spatter?
Excessive amperage or incorrect polarity can lead to more spatter. Adjust current and ensure correct settings for electrode type.
What size welding cable should I use?
For high current machines like the EWELDS315, use heavy-duty welding cables (at least 25mm² or larger depending on length).
What safety precautions should I take when welding?
Always wear a welding helmet, gloves, long sleeves, and ensure proper ventilation. Disconnect power before maintenance.
Reviews
There are no reviews yet.