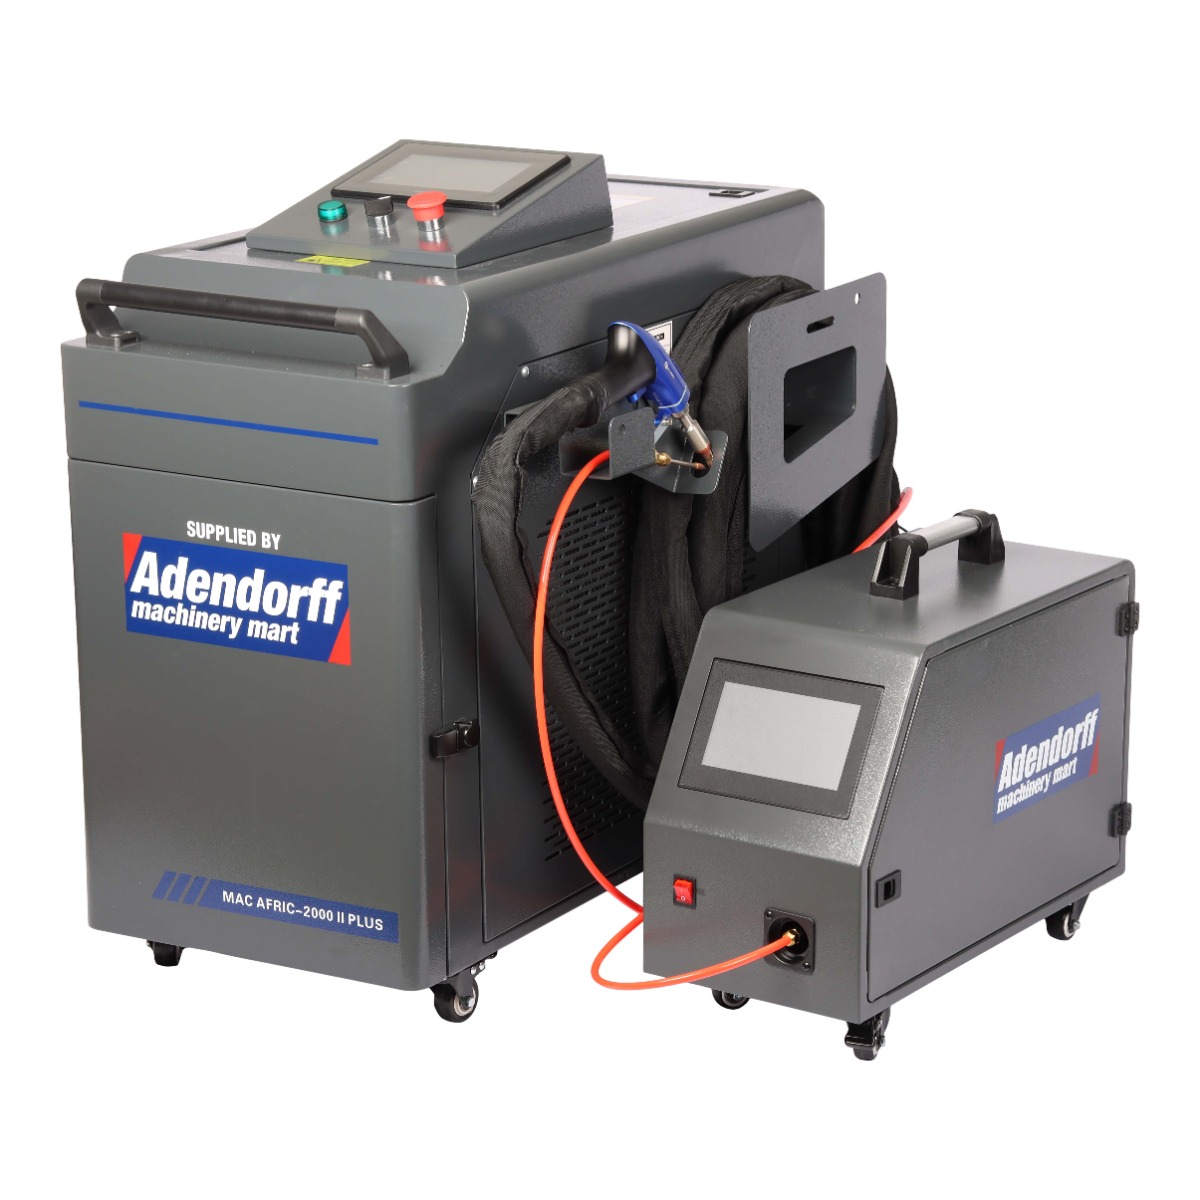
Mac Afric Hand-Held Laser Welding Machine, 2000W Air Cooled
The Mac Afric Hand-Held Laser Welding Machine, 2000W Air Cooled, delivers high-precision welding with a fiber length of 10M and a speed of up to 120mm/s. Ideal for industrial applications requiring strong, clean welds.
Description
Technical Specifications
Laser Power: 2000 W+
Laser Wavelength: 1080 ± 10 nm
Fiber Length: 10 m
Operate Mode: Continuous / Modulation
Welding Speed: 0 – 120 mm/s
Cooling System: Industrial Constant Temp Tank
Working Environment Temp Range: 10°C to 40°C
Working Environment Humidity: Up to 70% (no condensation)
Welding Thickness: 0.5 – 5 mm
Welding Gap Requirements: 0.5 mm
Working Voltage: 220 V 50 Hz
Performance & Features
FeatureDetails
Operation Modes: Supports both continuous wave and modulated operation.
Welding Speed & Efficiency: Up to 35% electro‑optical efficiency; speeds 3–5× faster than traditional methods—higher productivity, lower cost per piece.
Shielding Gas: Pure nitrogen or pure argon.
Weld Joint Types: Butt, lap, corner welding.
Duty Cycle: Continuous 24‑hour operation supported.
Operational & Safety Considerations
AspectDetails
Built‑in Safety: Safety ground clamp required—laser emits only when clamp is attached and gun trigger is pressed.
Durability & Maintenance
ComponentReplacement Interval
Protective Lens: Replace monthly, depending on usage.
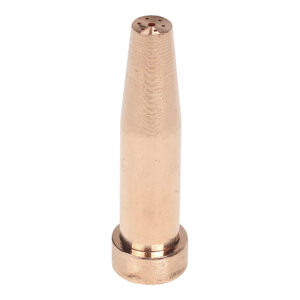
Copper Welding Nozzle: Replace every 3–5 months, depending on use.
Safety Precautions
Always wear full PPE: welding helmet with proper shade, laser-rated eye protection, gloves, long sleeves, and safety boots.
Ensure correct input supply: 220V single-phase.
Keep cooling system filled (if water-cooled).
Do not look directly at the laser beam.
Use clean, dry compressed air for plasma mode.
Ensure proper earthing and grounded workpiece.
Troubleshooting Guide
IssueLikely CauseSolution
Machine Does Not Power On: No mains power, blown fuse, faulty switch: Check supply, reset breaker, test switch
No Laser Output: Interlock not engaged, dirty lens, wrong settings: Check interlocks, clean lens, reset parameters
Weak or Unstable Arc: Low power, dirty workpiece, poor grounding: Increase power, clean metal, secure clamp
Plasma Torch Won’t Ignite: Low air pressure, worn tip, bad trigger: Ensure 4.5–6 bar pressure, replace parts, check trigger wiring
Excessive Dross (Plasma): Wrong speed, worn tip, bad air pressure: Adjust speed, replace tip, reset pressure
Machine Overheating: Duty cycle exceeded, clogged vents: Let cool, observe duty cycle, clean vents
Recommended Laser Welding Settings
MaterialThicknessEWELDL150EWELDL200Notes
Mild Steel: 0.8–1.5 mm: 40–60% power: 50–70% power: Single pass, thin sheets
Mild Steel: 2–3 mm: 60–80% power: 70–90% power: Pre-clean surface
Stainless Steel: 1–2 mm: 50–70% power: 60–80% power: Pulsed mode recommended
Stainless Steel: 3–4 mm: 70–90% power: 80–100% power: Multi-pass if needed
Aluminium: 1–2 mm: 50–70% power: 60–80% power: Stable hand movement required
Aluminium: 3–4 mm: Near max: 80–100% power: Prefer EWELDL200
Recommended Plasma Cutting Settings
MaterialThicknessEWELDL150EWELDL200Air PressureNotes
Mild Steel: 1–3 mm: 20–30 A: 25–35 A: 4.5 bar: Smooth sheet cutting
Mild Steel: 4–6 mm: 30–40 A: 40–50 A: 5.0 bar: Clean edges
Mild Steel: 8–10 mm: 40–50 A: 50–70 A: 5.5 bar: 150 at limit
Mild Steel: 12–16 mm: Not recommended: 70–90 A: 6.0 bar: Use EWELDL200
Stainless Steel: 3–6 mm: 25–40 A: 40–60 A: 5.0 bar: Slower feed
Aluminium: 3–8 mm: 25–40 A: 40–60 A: 5.5 bar: Steady arc
Key Notes
Both units are single-phase, portable, and workshop-friendly.
EWELDL150: Lower max output → best for thin to medium sheet metal, lighter laser welding.
EWELDL200: Higher output → thicker material capacity, longer duty cycle, more stable arc for plasma cutting and laser welding.
Reviews
There are no reviews yet.